
By Dr Palma González García
Simple changing fuel might look straightforward on paper. But our experience shows it affects the whole process, operator decision making and the case for investment. Here are six practical lessons we’d like to share.
(1) Instrument reading was a big surprise
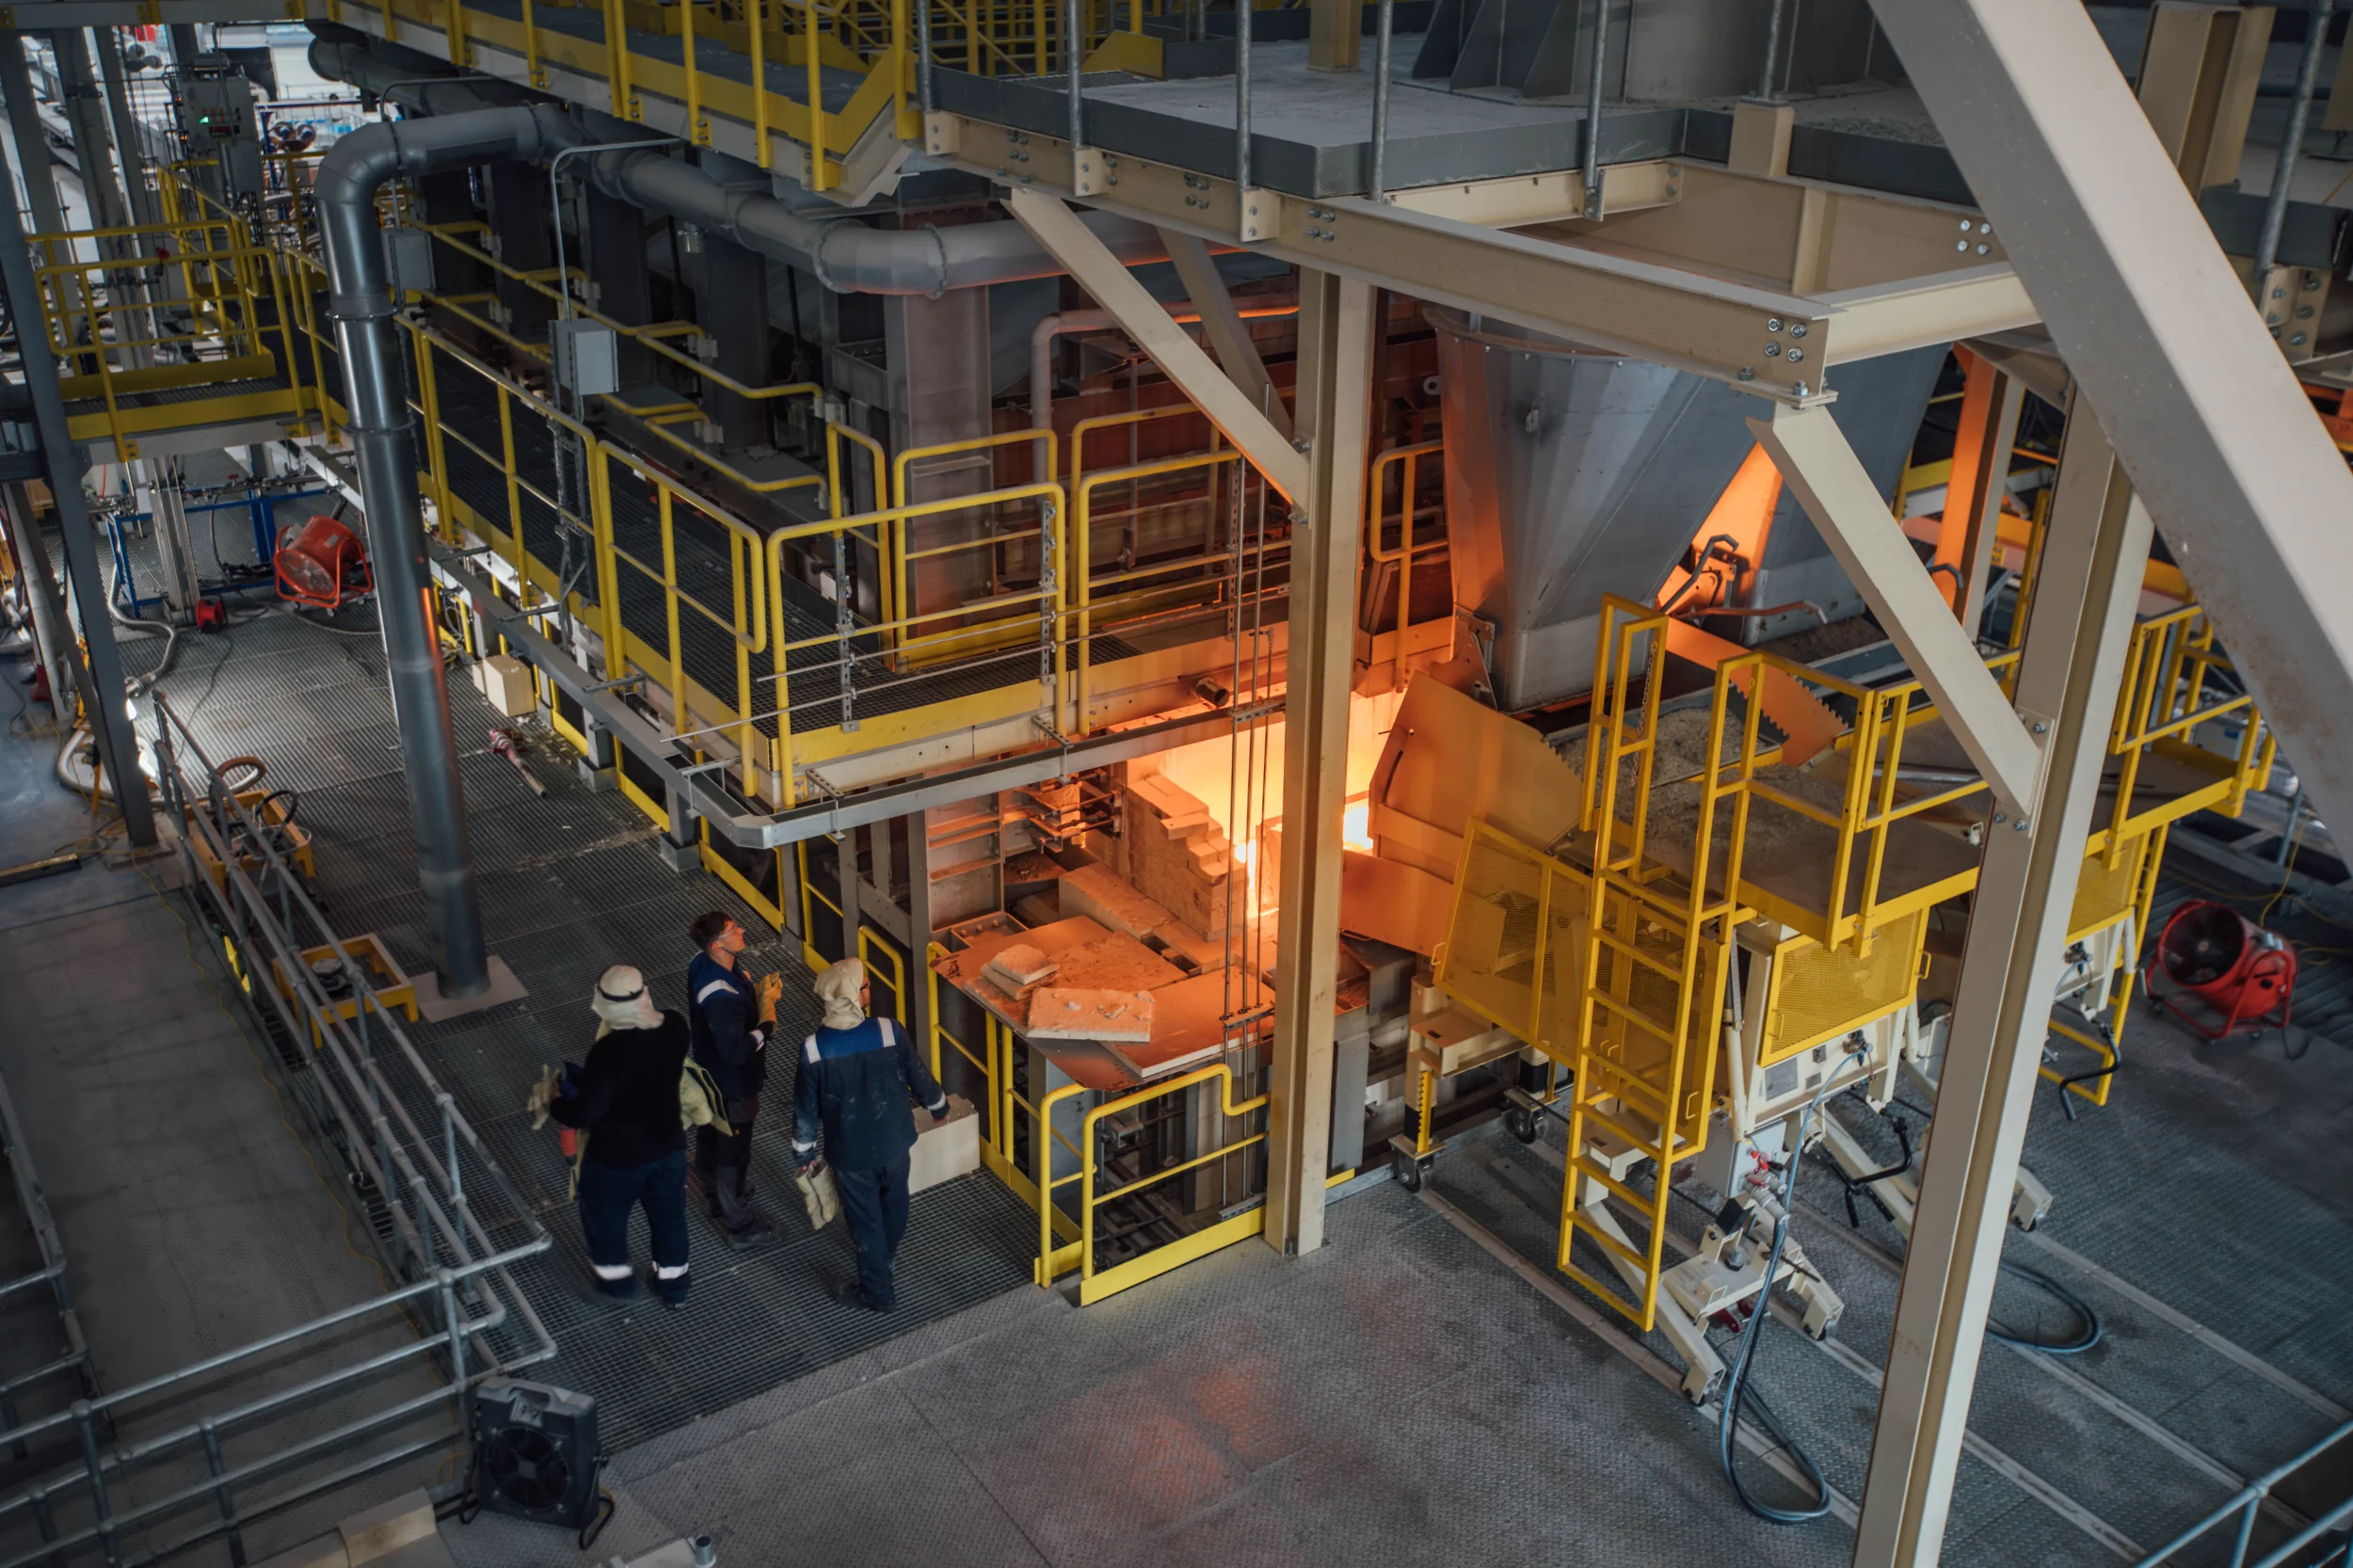
Fuel switching sounds straightforward, until it meets a real furnace. During a hydrogen trial the discussion in the control room wasn’t about flame temperature, emissions or energy efficiency. It was about instrument reading, which might sound surprising. The fuel was behaving largely as expected but the challenge was how we as operators could interpret a familiar measurement under unfamiliar conditions. Whether existing procedures remained appropriate and what was a normal response. Our discussion quickly shifted from combustion science to operational confidence, which we’ll cover later.
That experience shows a recurring lesson from our industrial fuel switching programmes. Replacing natural gas with hydrogen, biofuels, electricity or a combination may look linear on paper, but a change in energy source doesn’t automatically deliver the intended carbon reduction. The outcome depends on how the alternative energy is produced and supplied, as well as how it affects heat transfer, process stability, process controls, maintenance, product quality and operator decision-making. Understanding these wider effects is essential if manufacturers are going to protect quality, output and equipment while building a credible case for investment.
(2) Combustion doesn’t prove process performance
A stable flame is an important milestone, but it doesn’t prove that the wider process will perform as required. Industrial furnaces depend on the interaction between fuel properties, burner configuration, heat transfer, controls and production demand. Changing the fuel can alter conditions elsewhere even when the flame looks acceptable and emissions remain within expectations.
Heat transfer is often where this complexity first becomes visible. Changes in flame luminosity, length, temperature distribution and momentum can alter where and how energy reaches the glass melt. A fuel may deliver the required total heat while still creating local hot or cold regions, uneven product heating or a narrower operating window.
Success must therefore be measured at process and product level. A strong carbon reduction result has limited value if it reduces throughput, affects quality, accelerates refractory wear or increases maintenance. Trials must assess the production response, not combustion data in isolation. Controls and instrumentation are part of the same assessment. Signals and alarm limits developed for conventional fuels may require different interpretation, recalibration or new procedures. Trials must test both the technology and the information available to those expected to operate it safely. Before testing begins, success needs to mean more than good combustion performance. It should cover health and safety, heat transfer, emissions, quality, throughput, control and equipment condition. This wider view produced more useful evidence when faced with the next challenge – scale.
(3) Scale changes everything and confidence grows at each stage
Lab and pilot testing are essential for understanding fuel behaviour and reducing uncertainty, but they can’t reproduce every interaction in a production furnace. As scale increases, geometry, thermal inertia, residence time, flow distribution, heat losses and control response all change. At full scale, the system has to work across longer pipework, multiple burners and existing site infrastructure. In glass making, a mixing pattern or flame momentum that looks acceptable on one burner can influence glass convection currents when repeated across the furnace. Controls must also respond to larger process volumes and slower feedback.
Industrial trials add production constraints such as protecting output and quality within limited test windows. Fuel supply, storage, pressure stability, changeover arrangements and compatibility with existing equipment must all be managed. These are important issues that determine whether a concept can function on a working site.
And different stages answer different questions. Models reveal sensitivities, controlled experiments isolate mechanisms, pilot trials bring equipment together and industrial demonstrations show what happens alongside production. Confidence grows when these layers support one another and their limitations are clear.
The key scale-up question is therefore what has been demonstrated under conditions relevant to the intended application and which assumptions remain untested. As trials approach production scale, success also depends on preparing the operators whose observations and decisions determine real-time performance.
(4) Operators are equally important as the technology and should inform trial design
Operators are as important to successful fuel switching as the technology itself. A technically sound system only delivers value when the people running the furnace feel confident using it safely and consistently. New flames, start-up sequences, control responses and alarms can make familiar decisions less straightforward, particularly during the first stages of a trial. This isn’t an operator shortcoming. Industrial knowledge is built around established signals and routines. When fuel properties change, procedures, alarm limits and decision trees must be reviewed alongside the equipment. Training should explain what has changed, which indicators remain reliable and when intervention is required.
Health and safety considerations must be embedded throughout trial planning and execution. For alternative fuels, fuel specific risk assessment and hazardous area requirements, together with isolation and emergency procedures must be reviewed, clearly defining operating limits and stop criteria. Leak detection strategies and ventilation arrangements must be also assessed and implemented as required. These control measures should be verified before fuel is introduced into the furnace and reinforced through operator training, pre-trial briefings and emergency response exercises. During trials, continuous monitoring and clear communication amongst operations, engineering and safety teams are essential to identify and address unexpected conditions promptly. Operator involvement is central to making these controls effective in practice.
Early operator involvement in trial design vastly improves outcomes. Operators can identify constraints that models and engineering documents can miss. Everything from response times, instrument clarity, isolation sequences and the point at which a nominally stable process becomes difficult to manage. Their practical experience should inform hazard reviews and help identify operational considerations that may affect trial planning and execution. Structured feedback is equally important. Shift debriefs, observations and intervention records can explain differences between runs, reveal where automation is needed and show when an operating point places too much demand on manual controls.
Operator readiness is therefore part of technology readiness and equally important. Procedures, training and control room changes need to be planned from the start, not added once the engineering is complete. Technology may enable the transition, but operators are the people who make it safe, repeatable and workable in practice.
(5) The best fuel depends on the furnace and the process needed
At Glass Futures we’re often asked which fuel or what technology will ‘win’. Hydrogen, biofuels, electrification or a hybrid approach. But our industrial experience points to a more useful question, what option fits best for the furnace, the site and the operating strategy.
Each option brings a different balance of opportunity and constraint. Hydrogen can reduce direct carbon emissions but changes flame behaviour, emissions, supply needs and safety considerations. Biofuels may feel more familiar to existing combustion systems, although consistency, contaminants and sustainable supply still matter. Electrification removes on-site combustion emissions, but its suitability depends on where the heat is needed, available grid capacity and the effect on glass convection currents and product quality.
The practical answer may be a hybrid system, using electricity where heat can be transferred efficiently and combustion where flame coverage, atmosphere control or flexibility remain important. This can improve resilience but also adds integration and control complexity.
Technology selection is best treated as a staged decision. Start with the process need. What is the required thermal profile, the product specification and the operating window. Then assess what the existing asset and site utilities can support safely and reliably. From there, distinguish between changes that can be introduced within the existing system, technologies that could be adopted through a targeted retrofit, and options better aligned with a furnace rebuild.
Hybrid solutions may be relevant across these pathways, depending on the asset, infrastructure and degree of integration required. Yet, choosing the pathway is only the first step. Before committing capital, manufacturers need evidence that it can deliver under the conditions that matter in practice.
(6) Success isn’t pass or fail, it’s evidence that brings investment
An industrial trial shouldn’t be reduced to a pass or fail result. They can’t remove every uncertainty, but they can replace the most important assumptions with evidence and reveal what remains unresolved. Decision-makers need to know what was tested, under which conditions, for how long and against which criteria. Safe operation during a short campaign is valuable evidence, but doesn’t by itself prove long-term reliability, maintenance demand, energy availability or commercial performance.
Trial objectives should therefore link to the decisions they must support. Relevant measures may include energy use, emissions, heat transfer, product quality, throughput, controllability, equipment condition and operator interventions. Negative or inconclusive findings have value when they expose assumptions, define operating boundaries or prevent premature commitment.
And interpretation matters as much as measurement. Results from one furnace or operating window cannot automatically be generalised. Data gaps, short durations and differences from commercial conditions must be explicit. Modelling can extend the evidence, but its predictions should remain anchored to measured performance and visible uncertainty. The investment case must include what is required around the technology such as infrastructure, controls, safety systems, maintenance capability, operator training, production disruption and contingency arrangements.
In summary
As these lessons show, changing the energy source means changing much more than the flame. Everything from combustion, scale and operator readiness to technology choice and investment evidence. They all need to work together if a furnace is to operate safely, reliably and productively.
Across industrial transformation, whatever sector we work in, the most useful thing we can do is to compare experiences, collaborate and share our failures and successes. Where are the greatest barriers emerging? What evidence is proving decisive, and can it be applied elsewhere? What didn’t work and why? It’s only by having these discussions that industry can learn faster and act confidently in decarbonisation and transformation.